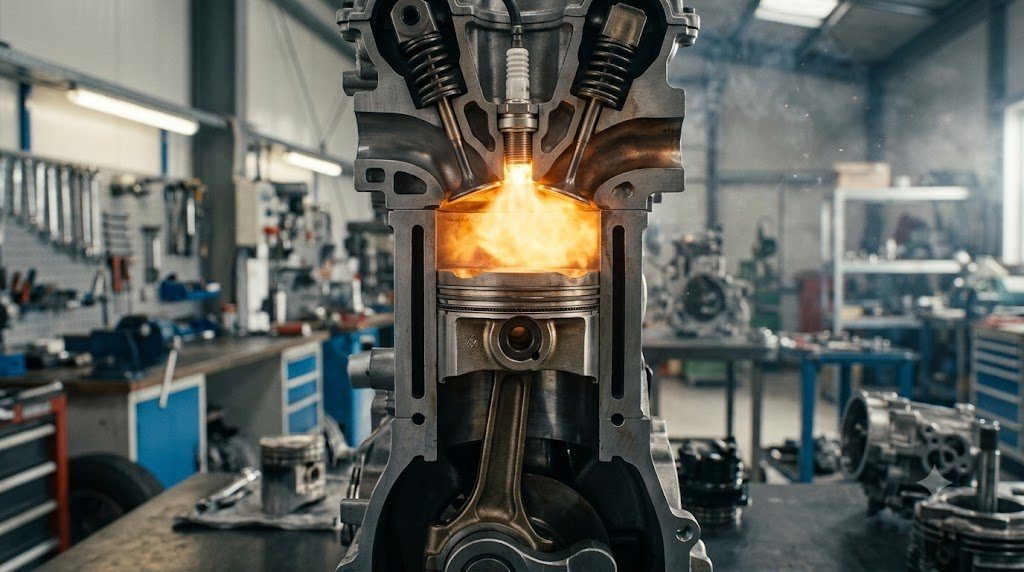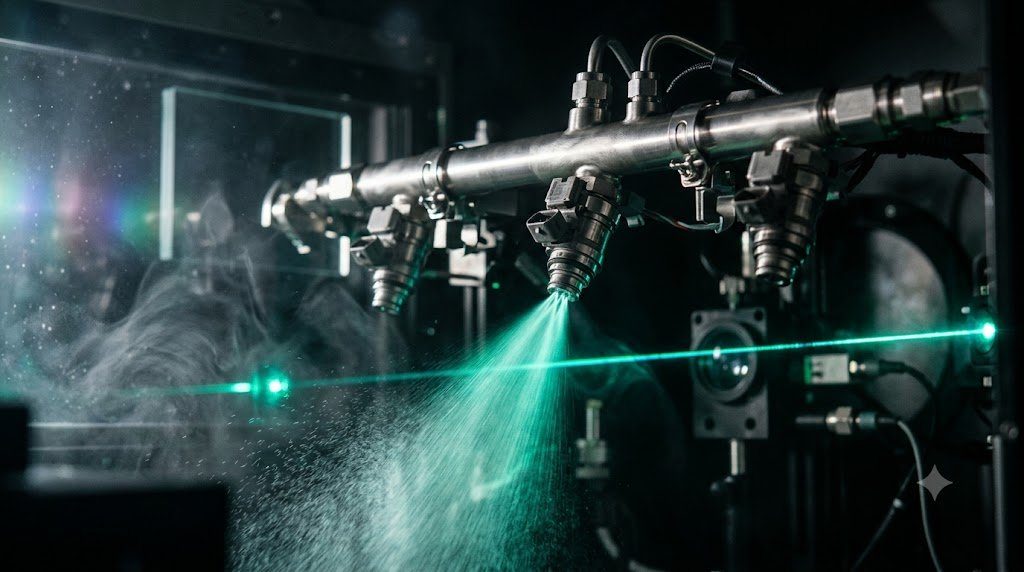
The transition from legacy port fuel injection (PFI) to Gasoline Direct Injection (GDI) represents the most impactful powertrain engineering advancement in spark-ignition engines over the past two decades. By spraying finely atomized gasoline droplets directly into the combustion chamber at pressures exceeding 200 to 350 bar (2,900 to 5,000 psi), GDI systems exploit the latent heat of fuel vaporization to cool the in-cylinder air charge, dramatically suppressing detonation and enabling higher geometric compression ratios with aggressive turbocharging boost pressures.
When liquid gasoline atomizes and evaporates directly within the closed cylinder bore, it absorbs latent heat of vaporization ($h_{fg} \approx 350 \text{ kJ/kg}$) directly from the compressed intake air mass. This in-situ phase change drops trapped charge temperatures by 15°C to 25°C at the point of ignition, allowing engine calibrators to advance spark timing toward Maximum Brake Torque (MBT) and increase base compression ratios by up to 1.5 full points without inducing destructive pre-ignition knock.
High-Pressure Fuel Rail Dynamics and Hydraulic Pump Architecture
A modern GDI fuel system comprises two distinct hydraulic pressure circuits: a low-pressure in-tank lift pump delivering fuel at 4 to 6 bar, and a camshaft-driven single-piston high-pressure fuel pump (HPFP) that elevates line pressure to 150-350 bar. The HPFP utilizes an internal electromagnetic spill valve modulated via pulse-width modulation (PWM) by the Engine Control Unit (ECU) to meter fuel volume entering the pumping chamber on every cam stroke.
The high-pressure fuel rail acts as a hydraulic accumulator, dampening severe pressure pulsations generated by alternating pump delivery strokes and rapid multi-hole injector openings. If rail volume is undersized, hydraulic standing pressure waves induce cylinder-to-cylinder fuel delivery variations exceeding 8%, causing localized lean misfires and unburned hydrocarbon spikes.
Multi-Hole Solenoid vs. Piezoelectric Outward-Opening Injectors
GDI fuel injectors operate under severe thermal and mechanical stresses, seated directly within the cylinder head deck between intake and exhaust valves where combustion temperatures exceed 2,000 K. Two primary injector actuation technologies dominate the market:
- Multi-Hole Solenoid Injectors: Utilize an electromagnetic coil to lift an internal needle off its seat against a heavy return spring. Fuel discharges through 5 to 8 laser-drilled micro-orifices (diameters between 100 and 160 μm) configured to generate an asymmetric spray cloud that avoids impinging on cylinder walls. Minimum opening response times range between 1.2 and 1.8 milliseconds.
- Piezoelectric Injectors: Utilize a stacked ceramic actuator that expands linearly by micrometers within 0.1 milliseconds when energized with 150-200 volts. Piezoelectric outward-opening pintle injectors produce hollow-cone fuel sprays with ultra-fine droplet sizes (Sauter Mean Diameter $SMD < 12 \, \mu\text{m}$), enabling up to five discrete injection events per single combustion cycle (split-injection strategies during cold start and stratified lean burn).
| Injector Technology | Operating Pressure Range | Actuation Response Time | Typical Sauter Mean Diameter (SMD) | Multi-Injection Capability |
|---|---|---|---|---|
| Port Fuel Injection (PFI) | 3.0 to 4.5 bar | 2.5 – 3.5 ms | 80 – 120 μm | Single Injection per Cycle |
| GDI Multi-Hole Solenoid | 150 to 250 bar | 1.2 – 1.8 ms | 15 – 25 μm | 2 – 3 Injections per Cycle |
| GDI Outward-Opening Piezo | 200 to 350 bar | 0.1 – 0.2 ms | 10 – 15 μm | Up to 5 Injections per Cycle |
| Common-Rail Diesel Solenoid | 1,800 to 2,500 bar | 0.3 – 0.5 ms | 8 – 14 μm | Up to 7 Injections per Cycle |
Wall Wetting, Piston Crown Impingement and Particulate Matter (PM)
Despite massive gains in thermal efficiency and torque density, GDI engines exhibit an inherent physical vulnerability: the formation of microscopic Carbon Particulate Matter ($PM_{2.5}$ and $PM_{10}$) and sub-23 nanometer solid particle numbers ($PN$). In a port-injected engine, fuel has ample time (several milliseconds) to mix thoroughly with intake air while washing past warm intake valves.
In a GDI engine, fuel is introduced during a fraction of a stroke (often less than 30 degrees of crankshaft rotation). If spray penetration is excessive, liquid droplets strike the relatively cold cylinder liner or piston crown—a phenomenon known as Wall Wetting. Trapped liquid fuel pools cannot evaporate before the flame front sweeps past; instead, the liquid pools burn via diffusion combustion, creating localized rich zones that pyrolyze into solid carbon soot particles.
Gasoline Particulate Filters (GPF) and Dual PFI/GDI Fuel Architectures
To meet stringent Euro 6d and EPA Tier 3 emissions standards, modern vehicle manufacturers deploy two engineering solutions:
- Gasoline Particulate Filters (GPF): Wall-flow ceramic honeycomb filters manufactured from cordierite or silicon carbide installed in the exhaust stream. As exhaust gases force through porous cell walls, soot particles are mechanically trapped and subsequently oxidized into $CO_2$ during high-temperature exhaust regeneration phases.
- Dual PFI/GDI Systems: Advanced engines combine both port and direct injectors per cylinder. Under low-load idling and suburban cruising, the engine operates exclusively on port injectors, ensuring homogenous mixing, zero wall wetting, and minimal particulate formation. When high torque or wide-open throttle is demanded, the ECU blends or transitions entirely to direct injection for knock resistance and peak power.
Sauter Mean Diameter (SMD) and Rayleigh-Taylor Droplet Breakup Physics
The physical quality of direct gasoline spray atomization is quantified by the Sauter Mean Diameter ($D_{32}$ / SMD)—the diameter of a droplet that possesses the identical volume-to-surface-area ratio as the entire spray cloud. High-pressure injection produces rapid droplet atomization through two cascading aerodynamic instability mechanisms:
First, the high-velocity fuel jet exiting the micro-orifice (velocities exceeding 150 to 250 m/s) undergoes primary atomization driven by Kelvin-Helmholtz surface wave shear instabilities against dense compressed cylinder air. Second, shearing droplets exceed the critical Weber number ($We = \rho_{air} v_{rel}^2 D / \sigma > 12$), triggering secondary Rayleigh-Taylor catastrophic aerodynamic breakup into microscopic droplets under $SMD < 15 \, \mu\text{m}$.
Intake Valve Carbon Deposit Formation: The Loss of Port Fuel Washing
A critical service issue unique to GDI engines is severe Intake Valve Carbon Accumulation. In legacy port fuel injected engines, detergent-additized gasoline sprayed continuously across the backside of intake valves, washing away oily residues carried by the Positive Crankcase Ventilation (PCV) system. In GDI engines, intake valves remain dry. Engine oil mist from the PCV system bakes onto scorching 200°C intake valve tulips, forming dense carbon crusts that choke cylinder airflow and disrupt intake tumble within 60,000 to 100,000 kilometers, necessitating walnut-shell media blasting.
Field Case Study: High-Pressure Fuel Pump Cam Follower Wear and Rail Loss
In popular 2.0-liter turbocharged GDI engines (such as early VAG EA113 and Ford EcoBoost platforms), the high-pressure fuel pump (HPFP) is driven off a specialized multi-lobe cam on the exhaust camshaft. To translate rotary cam motion into linear pump piston travel, early designs utilized a flat case-hardened steel bucket follower.
Due to intense spring forces (exceeding 800 N) and extreme contact pressures, inadequate engine oil film retention or extended oil change intervals caused the diamond-like carbon (DLC) coating on the follower to abrade. Once through the hardened coating, the cam lobe machined completely through the steel bucket within thousands of kilometers, driving the hardened pump plunger directly against the camshaft lobe.
Oscilloscope Diagnostic Waveform Analysis of HPFP Spill Solenoids
Master technicians diagnosing low rail pressure DTCs (P0087) connect a dual-channel oscilloscope to the HPFP spill control solenoid and high-pressure rail sensor. A healthy system exhibits a sharp current ramp (peaking at 6.5 Amps) followed by a sharp hydraulic pressure rise on each cam stroke. A worn pump follower or sticking spill valve exhibits delayed pressure rises and current flutter, confirming mechanical hydraulic loss before physical cylinder head disassembly.
Standardized Workshop Inspection Protocols and Factory Assembly Tolerances
Professional automotive service and certified powertrain remanufacturing adhere strictly to standardized workshop procedures defined by the Society of Automotive Engineers (SAE International), the International Organization for Standardization (ISO), and OEM factory workshop manuals. Rebuilding modern vehicle subsystems requires rigorous mechanical measuring tools, calibrated digital torque-to-yield angle meters, and ultra-clean workshop assembly cleanrooms.
When assembling high-precision automotive components—such as crankshaft main journal bearings, transmission planetary carriers, high-pressure fuel injectors, or multi-piston brake calipers—technicians enforce strict cleanliness standards governed by ISO 16232 (Road Vehicles – Cleanliness of Components and Systems). Component parts must be washed in ultrasonic cleaning tanks using solvent degreasers, dried with filtered compressed air, and inspected under particulate optical microscopes to verify that residual metallic particles do not exceed 200 micrometers.
Torque-to-Yield (TTY) Fasteners and Ultrasonic Bolt Tension Measurement
Critical powertrain and chassis joints—such as cylinder head bolts, connecting rod cap bolts, flywheel bolts, and suspension knuckle fasteners—universally utilize Torque-to-Yield (TTY) Fasteners. Unlike standard elastic bolts that operate within their linear elastic region, TTY bolts are tightened past their proportional limit into plastic deformation, providing constant clamp load despite thermal expansion cycles.
Technicians must utilize calibrated digital torque-angle wrenches: the fastener is first tightened to a specified initial snug torque (e.g., 40 Nm), followed by one or two precise rotational angle sweeps (e.g., +90° +90°). Because TTY fasteners undergo permanent plastic elongation, they are strictly single-use components; reusing a stretched TTY fastener risks catastrophic bolt necking and fastener shear under high cylinder pressure.
Comprehensive Workshop Maintenance and Tolerance Inspection Matrix
| Inspection Parameter / Task | Governing Standard / Tool | Allowable Workshop Tolerance | Critical Diagnostic Action Required |
|---|---|---|---|
| Bearing & Journal Clearances | Plastigage / Precision Micrometers | 0.025 to 0.050 mm (0.0010 – 0.0020 in) | Select undersize/oversize selective bearings |
| Cylinder Bore Taper & Out-of-Round | Dial Bore Gauge (Three Axis) | < 0.012 mm (0.0005 in) Maximum | Precision CNC plateau hone or overbore sleeve |
| Brake Rotor Lateral Runout | Dial Indicator on Magnetic Base | < 0.038 mm (0.0015 in) Assembled | Index rotor on hub or machine with on-car lathe |
| Wheel Hub Bearing Endplay | Dial Indicator Axial Deflection | < 0.050 mm (0.0020 in) Axial Play | Replace integrated hub bearing unit if exceeded |
| CAN Bus Static Resistance | Digital Multimeter (Pins 6 & 14) | 59.0 to 61.5 Ohms Balanced | Inspect 120-ohm terminating resistors & splices |
Adherence to these rigorous dimensional tolerances, factory torque tightening angles, and certified testing standards guarantees that serviced vehicle subsystems operate with original equipment factory reliability, thermal endurance, and maximum occupant safety throughout their operational lifecycle.
International Engineering Standards, Regulatory Audits and Quality Compliance
The engineering validation, roadworthiness certification, and manufacturing quality of motor vehicles are governed by stringent international regulatory treaties and engineering standards. Across major global automotive markets—predominantly the United States Federal Motor Vehicle Safety Standards (FMVSS), European Union Whole Vehicle Type Approval (EU WVTA / UNECE Regulations), and ISO 26262 Road Vehicles Functional Safety—every powertrain, chassis, and electronic subsystem must prove compliance through exhaustive durability and laboratory crash tests.
ISO 26262 Automotive Safety Integrity Level (ASIL) Classifications
Modern software-defined vehicles integrate safety-critical electronics under the rigorous framework of ISO 26262. Subsystems are categorized into Automotive Safety Integrity Levels ranging from ASIL-A (lowest hazard) to ASIL-D (highest safety criticality) based on three risk factors: Severity of injury ($S$), Exposure probability ($E$), and Driver Controllability ($C$):
- ASIL-D Subsystems (Zero-Tolerance Failure): Brake-by-wire modulators, Electronic Stability Control (ESC), Electric Power Steering (EPS), and High-Voltage Battery Disconnect Units (BDU). Mandates dual lockstep microcontroller cores, redundant hardware power feeds, and automated failure detection within 10 to 20 milliseconds.
- ASIL-C Subsystems: Electric traction motor torque control and transmission electronic shift-by-wire interlocks.
- ASIL-B Subsystems: Adaptive cruise control (ACC), lane departure warning, and active suspension dampening.
Global Emissions Regulatory Roadmaps: EPA Tier 3, Euro 6d and Euro 7
Internal combustion engines, direct injection fuel systems, and hybrid powertrains are subjected to continuously tightening exhaust emissions legislation. Under Euro 6d-ISC-FCM and forthcoming Euro 7 standards, vehicles must prove real-world emissions compliance on public highways using portable emissions measurement systems (PEMS) across ambient temperatures from -10°C to +38°C:
- Nitrogen Oxides ($NO_x$): Limited to less than 60 mg/km (gasoline) and 80 mg/km (diesel) through combined Selective Catalytic Reduction (SCR) with AdBlue urea injection and cooled low-pressure EGR loops.
- Solid Particle Number ($PN_{10}$): The regulatory measurement threshold has been tightened from 23 nanometers down to 10 nanometers, mandating wall-flow Gasoline Particulate Filters (GPF) across all turbocharged GDI engines.
- On-Board Fuel Consumption Monitoring (OBFCM): Standardized telemetry logging real-world lifetime fuel and electrical energy consumption directly within the engine ECU for regulatory transparency.
By anchoring design methodologies to these internationally recognized SAE, ISO, and UNECE standards, automotive engineers and diagnostic practitioners ensure that mechanical components deliver peak operational reliability, environmental compliance, and life-saving occupant protection.
Combustion Chamber Fluid Mechanics, Tumble Flow and Thermodynamic Boundary Layers
In the thermodynamic optimization of internal combustion engines, the geometric architecture of the cylinder head combustion roof exerts direct control over flame propagation speed and thermal heat losses. Modern direct-injection four-valve pent-roof combustion chambers are engineered to generate high-velocity Intake Tumble Flow—a coherent barrel-shaped vortex of air rotating perpendicularly to the cylinder axis.
As the piston accelerates upward on the compression stroke toward Top Dead Center, geometric squish pads on the piston crown compress this large tumble vortex, breaking it down into a cascade of fine, high-intensity microscopic turbulent eddies. This microscopic turbulence increases the Turbulent Flame Speed ($u_t$) by a factor of four compared to laminar flame speeds ($u_l$), completing combustion in fewer crank angle degrees and allowing significant spark retard reduction.
Piston Ring Tribology and Blow-by Hermetic Gas Sealing
Reciprocating pistons rely on three precision-engineered piston rings running inside plateau-honed cylinder liners to maintain gas hermetic sealing while controlling oil consumption: the Top Compression Ring, the Second Scraper Ring, and the Three-Piece Oil Control Ring. The top compression ring—manufactured from nodular cast iron or stainless steel with physical vapor deposition (PVD) diamond-like carbon (DLC) coatings—utilizes cylinder gas combustion pressure entering behind the ring groove to force the ring face tightly against the cylinder wall. Minimizing blow-by past the ring gaps to under 15 to 25 liters per minute prevents crankcase pressurization, preserves oil quality, and eliminates hydrocarbon emissions leakage.

Lead Automotive Research Engineer, Master ASE Certified Diagnostic Specialist, and powertrain dynamics consultant with over 18 years of experience in internal combustion thermodynamics, electric vehicle architectures, and chassis control systems.